Applications
Final chromium trim after argon-oxygen decarburization (AOD) for super-low-carbon austenitic grades such as 304L and 316LChromium additions in carbon-controlled 400-series ferritic and martensitic grades, where the alloy's own carbon content is the defining chemistry parameterStable chromium platform additions for heat-resisting alloys used in furnace hardware, automotive exhaust systems, and high-temperature structural serviceTwo-stage stainless practice generally: bulk chromium economically via high-carbon FeCr in the EAF, final trim via LC FeCr after decarburization
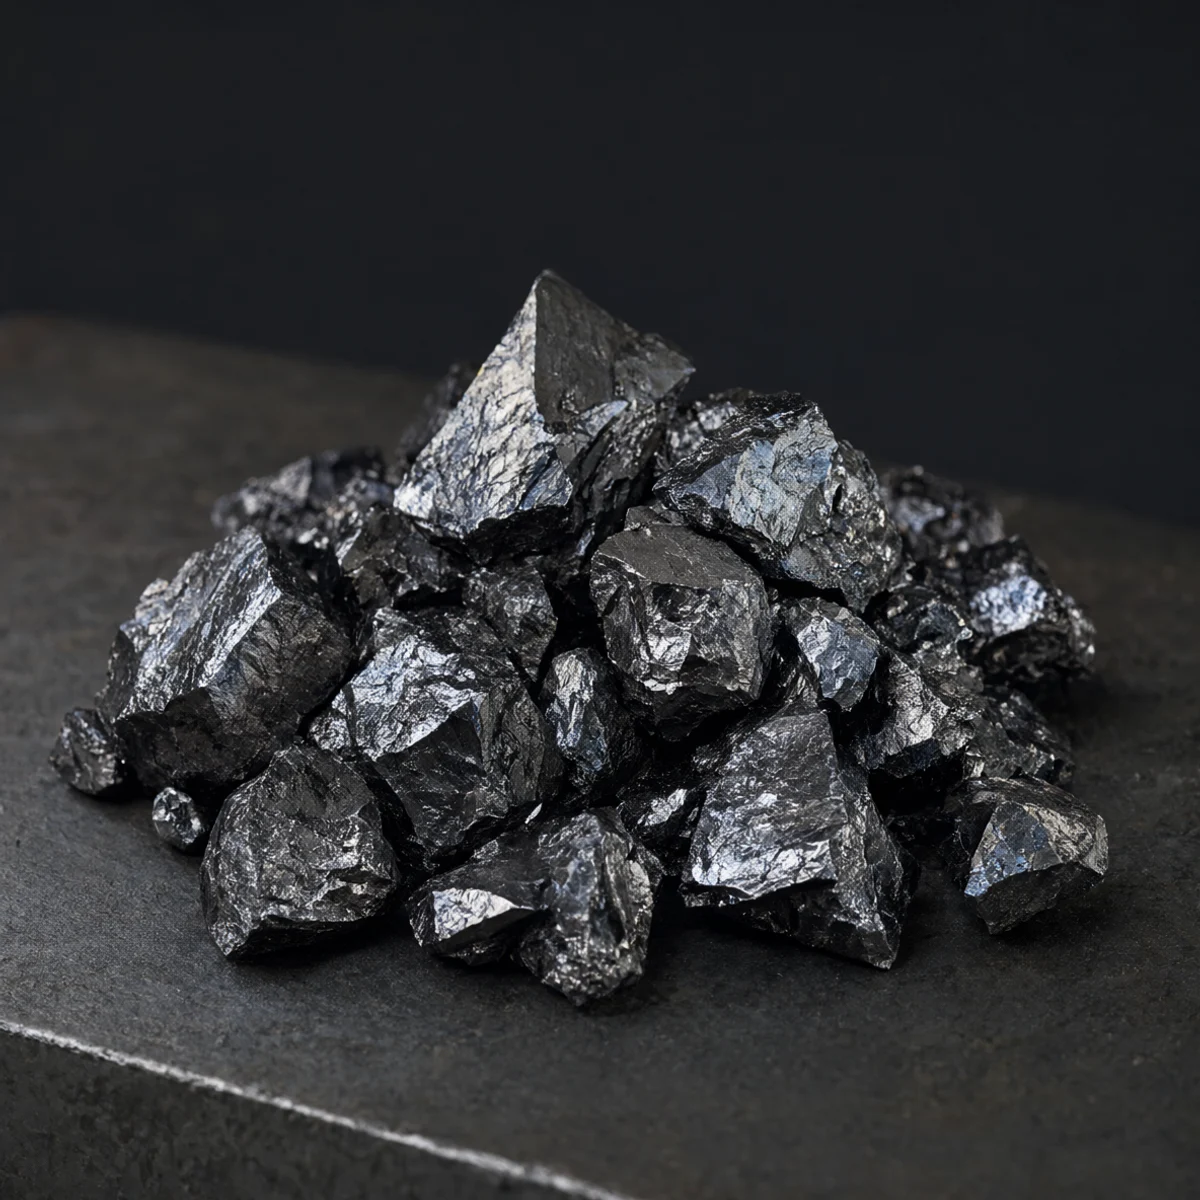
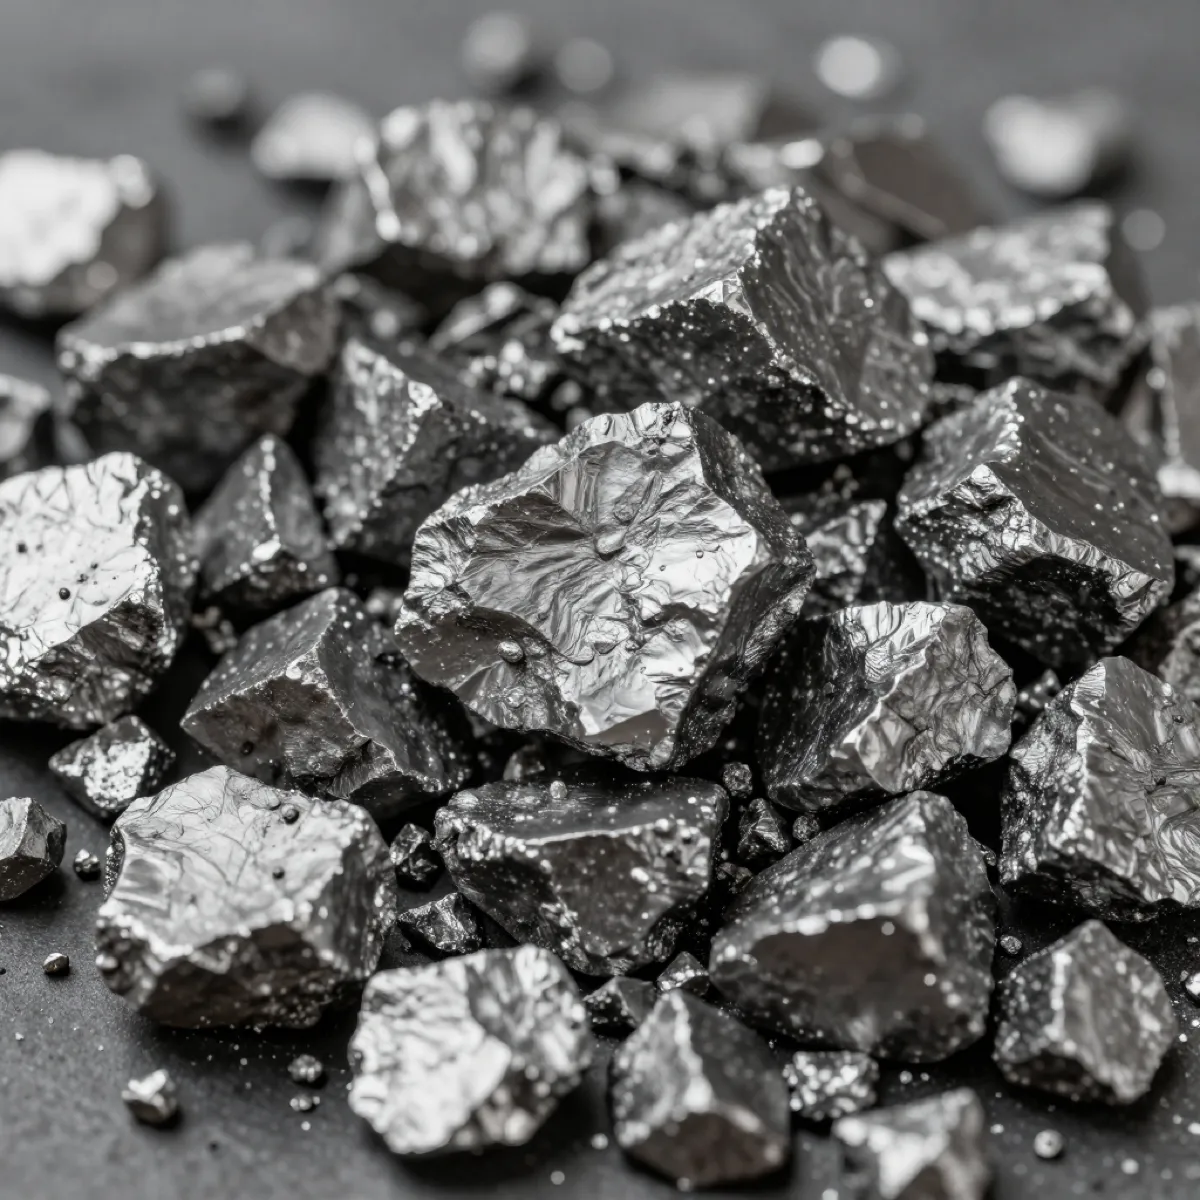
Ferrochrome is the primary chromium carrier in stainless and heat-resisting steel production, supplying the chromium that gives these alloys their corrosion resistance, high-temperature strength, and passivation behavior. It is produced by the carbothermic reduction of chromite ore in submerged arc furnaces, and it is supplied in two grades that bracket the carbon range demanded by modern stainless practice: high-carbon ferrochrome (HC FeCr, 4–8% carbon), which carries the bulk of the chromium charge economically, and low-carbon ferrochrome (LC FeCr, 0.03–0.5% carbon), which is reserved for the final chromium trim after decarburization. Both carry 60–70% chromium with controlled silicon and tight phosphorus and sulfur limits; what separates them — and what separates LC FeCr from the higher-carbon grade in cost — is how much of the carbon from the reduction is left in the alloy, and the refining steps required to get it out. LC FeCr is the grade specified where the heat’s final carbon is a specification, not a target.
The stainless route that created the need for LC FeCr is the standard two-stage EAF–AOD practice. In the electric arc furnace, the HC FeCr charge is melted with scrap under a reducing slag, and chromium recovery into the bath exceeds 95% when the silicon and aluminum residuals and the slag chemistry are well controlled. The heat is then transferred to the argon-oxygen decarburization (AOD) converter, where the defining problem of stainlessmaking appears: carbon must come down to the target specification without oxidizing excessive chromium into the slag. Argon dilution solves this by progressively lowering the CO partial pressure, so the carbon-oxygen reaction is favored over chromium oxidation and carbon can be driven down while most of the chromium stays in the bath. The AOD can economically take carbon to roughly the 0.05–0.08% range; pushing below that — to the 0.03% maximum of super-low-carbon grades such as 304L and 316L — becomes progressively more expensive in argon, time, and reduced chromium yield. The standard solution is not to force the AOD to do the whole job: the heat is taken to the economic decarburization limit, and the remaining chromium requirement is then trimmed with LC FeCr, whose 0.03–0.5% carbon cannot push the finished chemistry over its carbon limit. A final silicon-based reduction — ferrosilicon working together with the chemistry of the FeCr charge — then recovers into the bath the chromium that was inevitably oxidized, restoring chromium to specification.
The grades served are the super-low-carbon stainless program itself. For the austenitic grades such as 304 and 316, the chromium target sits near 18%, with ferromolybdenum supplying the 2–3% molybdenum that distinguishes 316 from 304 and provides pitting resistance; for the ferritic and martensitic grades of the 400 series (410, 430), chromium runs from roughly 11% to 17% and carbon control becomes the defining chemistry parameter — which is what makes the LC FeCr trim and a well-managed decarburization cycle essential. Heat-resisting alloys for furnace hardware, automotive exhaust systems, and high-temperature structural service depend on the same stable chromium platform, often combined with silicon and aluminum for oxidation resistance. In every case the impurity ceilings of the charge matter as much as the chromium itself: phosphorus and sulfur carried in by the FeCr cause embrittlement and hot shortness in the finished stainless — defects that are impossible to remediate downstream — which is why the material is held to 0.03% phosphorus or less and 0.04% sulfur or less.
Chromium yield is where the quality of the LC FeCr lot shows up in the cost of the heat, so the supply discipline is part of the specification. The material is screened to a controlled 10–50 mm lump range, with a 3–10 mm crushed grading available for specific charging systems, and every shipment carries certified chemistry within tolerance ranges that let the melt shop charge to aim rather than to a safety margin. Incoming lots are inspected for certified chemistry, lump sizing, and freedom from slag inclusions — because yield variability heat-to-heat is most often traced to inconsistent lump sizing, slag entrainment in undersized material, or chemistry drift in the silicon and carbon residuals, and each of those forces the over-addition that inflates alloy cost. The two grades are stored in segregated bins: HC FeCr and LC FeCr must never be mixed, and a carbon error from the wrong bin contaminates exactly the heats that can least afford it. For stainless mills running integrated EAF–AOD routes, a long-term supply relationship with consistent chemistry and a reliable HC FeCr / LC FeCr split is one of the most effective levers for stabilizing chromium yield, controlling alloy cost, and meeting the carbon specification on every heat. KHAKI TRADING CO., LIMITED supplies low-carbon ferrochrome within a portfolio of 32 product categories serving over 80 countries, with certificates of analysis and technical support available in 17 languages to match mill procurement and metallurgical requirements.
Need pricing or technical confirmation?
Send your application, grade, size, and quantity requirements by email for a faster response.
Request a Quote